3D Print Troubleshooting: Find the Fault by What You Can See
LayerWalker is a participant in the Amazon Services LLC Associates Program. We may earn a commission when you buy through links on our site, at no extra cost to you.
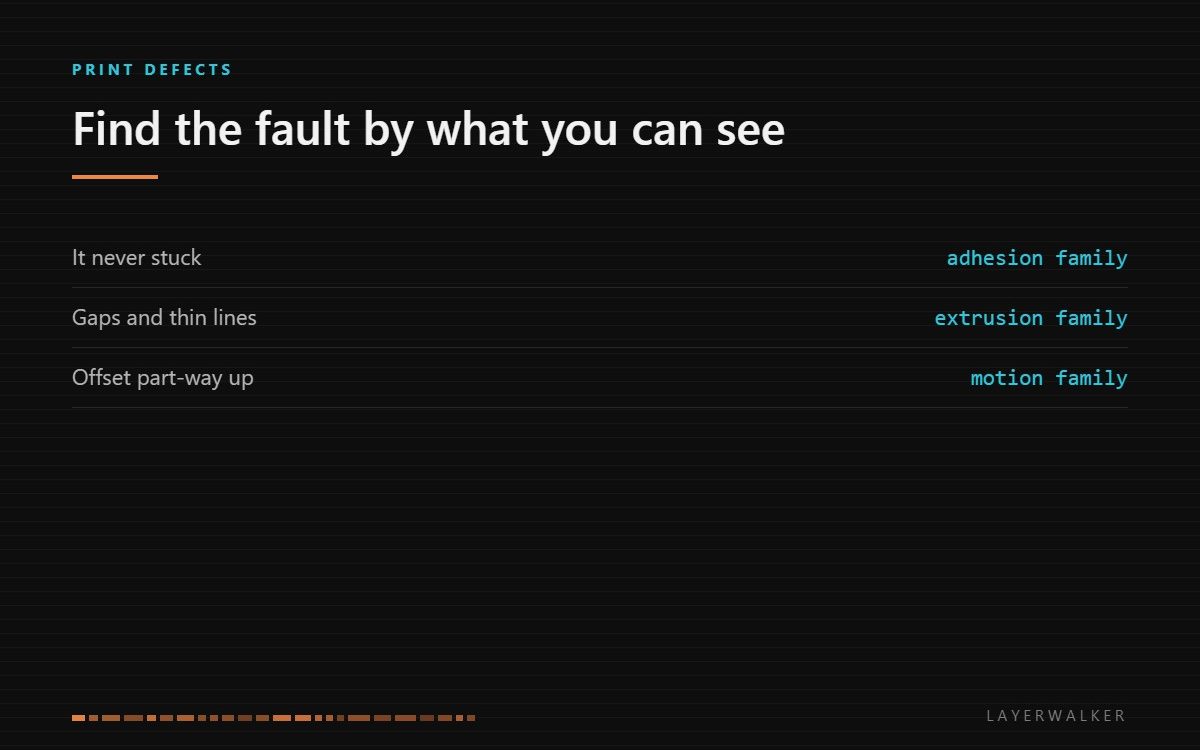
Work from the symptom, not the cause. Nearly every FDM fault falls into four families: it did not stick, it did not extrude right, the machine moved wrong, or the surface finished badly. Identify the family first and you skip most of the guesswork.
Where to buy


What to look for
Three cheap things diagnose most of what follows. A tool kit with nozzle needles, tweezers and hex keys covers the physical work, and the needles in particular settle the clog-or-not question in a minute. A digital caliper turns “it looks small” into a number, which is the difference between tuning flow and guessing at it. A multimeter matters once a fault is electrical rather than mechanical: heater and thermistor faults both read clearly on one, and both look identical from the outside.
Nothing else on this page needs buying. The fixes are settings, cleaning, and occasionally a part you already have a spare of.
Start with the family
| What you see | Family | Go to |
|---|---|---|
| Part lifts, curls or never grips the plate | Adhesion | first layer not sticking, warping |
| Gaps in walls, thin lines, missing material | Extrusion | under extrusion, clogged nozzle |
| Part is offset part-way up, or ends as a nest | Motion | layer shifting, spaghetti |
| Hairs, blobs, ripples, banding on the surface | Surface | stringing, blobs and zits, ringing, z banding |
| Part splits along layer lines under load | Bonding | cracking and delamination |
| Overhangs droop, bridges sag, supports fuse on | Geometry | overhangs and bridging, supports stuck on |
| Base spreads wider than the model | First layer | elephant foot |
Two questions before you change anything
First: is the filament dry? Moisture causes stringing, poor layer bonding, rough surfaces and popping noises, and it mimics at least four unrelated faults. A spool that has sat open for a month in a humid room will produce symptoms that no setting fixes. Dry it before you tune anything, or you will tune around a problem that is not there.
Second: did this machine ever print this file correctly? A fault that appeared suddenly is mechanical or environmental, and the list is short: a loose belt or grub screw, a plate that needs cleaning, a fan that has stopped, a room that got colder. A fault that has always been there is a settings or slicer problem, and belongs in the calibration sequence rather than the repair one.
Change one thing at a time
The most expensive mistake in troubleshooting is adjusting three settings at once and getting a better print. You have learned nothing, and the next failure starts from zero. Change one variable, print the same test, and write down what happened. It feels slower for two prints and is faster from the third onward.
Keep the test small. A full-size part takes hours to tell you what a twenty-minute coupon tells you, and most faults show themselves in the first few centimetres. Where a fault only appears at height, that is itself a clue: it points at thermal drift, a Z axis problem, or filament running out of a tangled spool, not at the first-layer settings people usually reach for.
When it is the machine, not the print
A few symptoms take you out of the slicer entirely. A printer that halts mid-job with a temperature error has an electrical fault in the heater or sensor circuit. A layer shift that repeats at the same height on the same model is usually the model; a layer shift at random heights is the machine. A grinding noise at the extruder with no filament moving means a blockage downstream, not an extruder that needs tightening.
For machines that report structured error codes, the code is far more useful than the symptom, because it tells you which subsystem the firmware itself believes has failed. Our error code pages work through those individually.
FAQ
Where do I start if the print fails immediately? Adhesion family. Clean the plate first, then check first layer height.
Where do I start if it fails part-way up? Motion or thermal. Check belts and grub screws, then whether the failure height is repeatable.
Can wet filament really cause this many problems? Yes, and it is the single most common hidden cause. Dry first, diagnose second.
How long should a test print be? Twenty minutes or so. If the fault does not appear in that, note the height at which it does.

LayerWalker
Print defect diagnosis, calibration procedures and parts that actually fit. Corrections welcome through the contact page.