3D Printer Retraction Settings: Distance, Speed, and What They Cannot Fix
What to look for Retraction is a setting, not a purchase, so the things worth buying are the ones that decide how…
OrcaSlicer, Bambu Studio, Cura and PrusaSlicer. What each setting actually changes, and the calibration order that makes the rest of the settings meaningful.
What to look for Retraction is a setting, not a purchase, so the things worth buying are the ones that decide how…
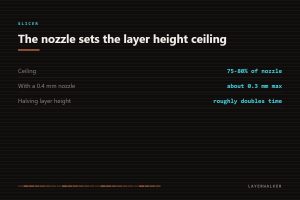
Layer height is capped at roughly 75 to 80 percent of nozzle diameter. Past that the bead cannot bond to the one below it.
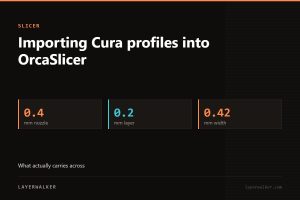
There is no direct importer. What transfers is your knowledge of the values, not the file.
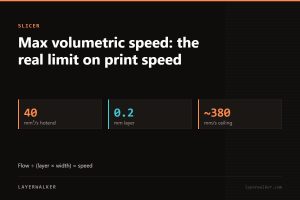
The hotend can only melt so much plastic per second. Above that limit the machine under-extrudes silently.
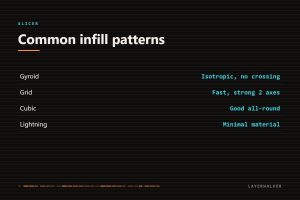
Gyroid for strength in every direction. Grid for speed. Below about 25 percent the pattern barely matters.
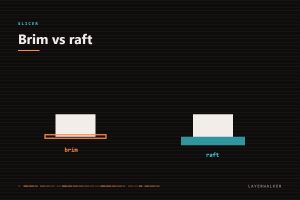
Brim for warping and small footprints. Raft almost never, unless the plate is beyond saving.
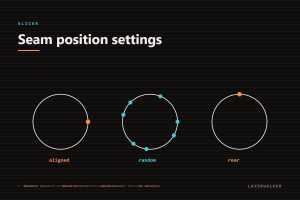
Aligned, random, rear or painted. Painted wins on anything you care about the look of.
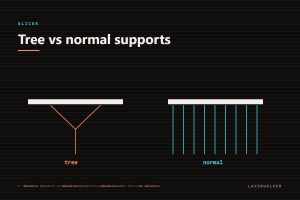
Tree supports touch in fewer places and use less material. Normal supports hold flat undersides better.
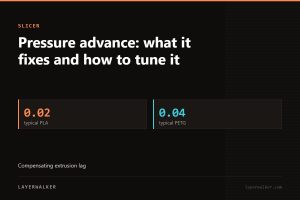
Corners with blobs, corners with gaps. Pressure advance fixes both because both come from the same lag.
Seven tests, one correct order. Running them out of sequence means tuning around errors you have not fixed yet.